Multicore Cables Manufacturers in India
Table of Contents
Introduction
Established in 2013 and headquartered in Rajkot, Gujarat (India), Megacab is a trusted name in the manufacturing, trading, and exporting of high-quality wires and cables. Built on a strong foundation of engineering excellence, innovation, and customer-first values, we deliver reliable electrical solutions that power homes, industries, and infrastructure across India and global markets.
Electricity plays an important role in every industry, commercial building, factory, and residential project. To transfer electrical power safely and efficiently, high-quality cables are required. Among the different types of electrical cables available in the market, multicore are widely used because they can carry multiple electrical conductors within a single outer sheath. They help simplify wiring, improve cable management, and support reliable electrical connections.
Today, the demand for Multicore Manufacturers in India is increasing because of the growth of industrial automation, infrastructure development, electrical equipment, and manufacturing industries. Businesses need that offer dependable performance, durability, and suitability for different working environments.
Megacab is a name to consider when looking for reliable cable solutions for industrial and electrical applications. By focusing on quality, performance, and customer requirements, Megacab aims to support businesses that need dependable cable products for their projects.
What Are Multicore Cables
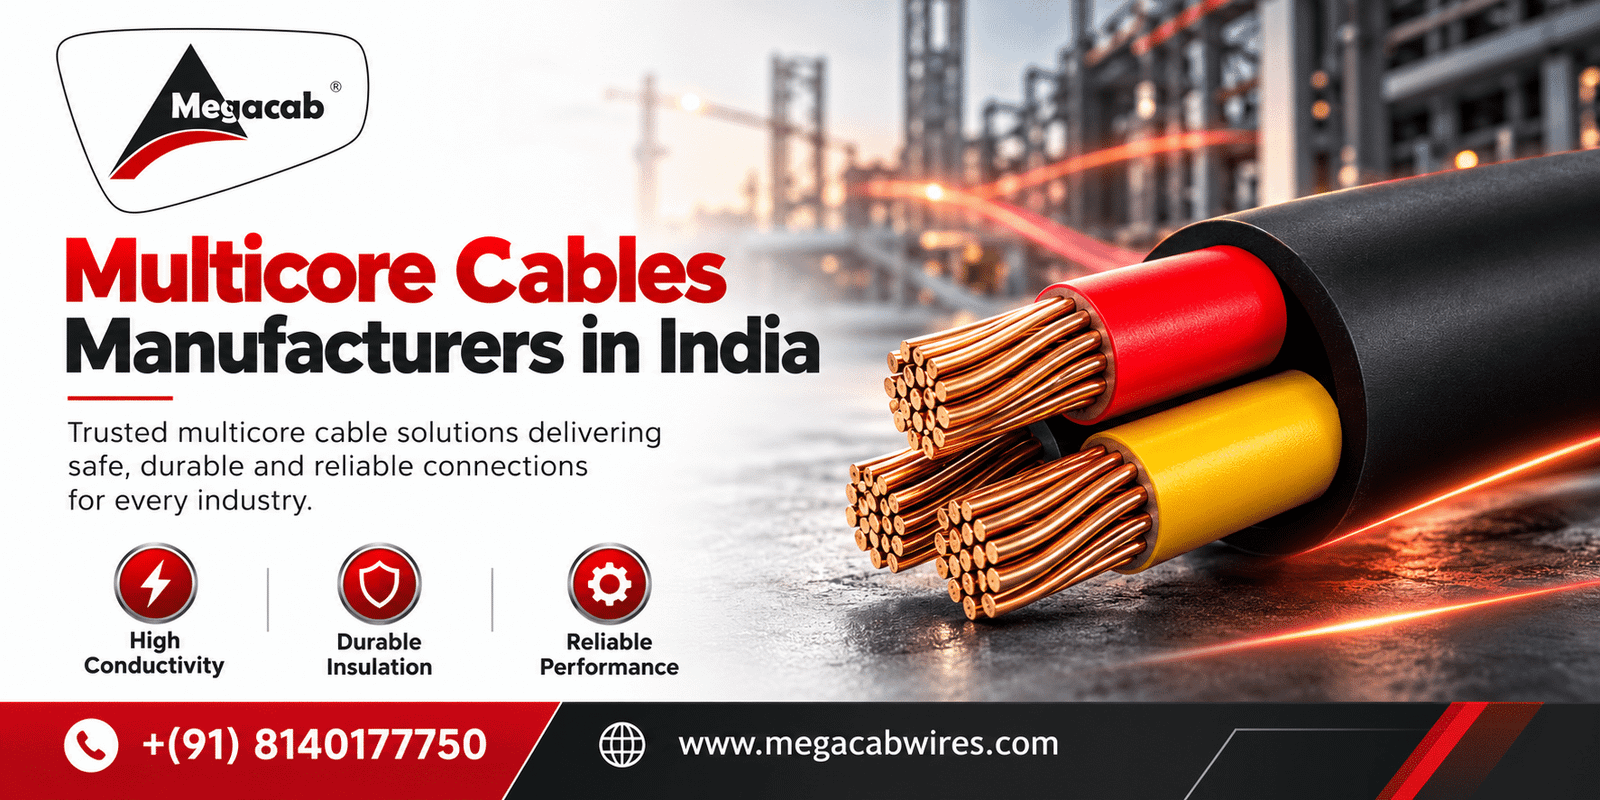
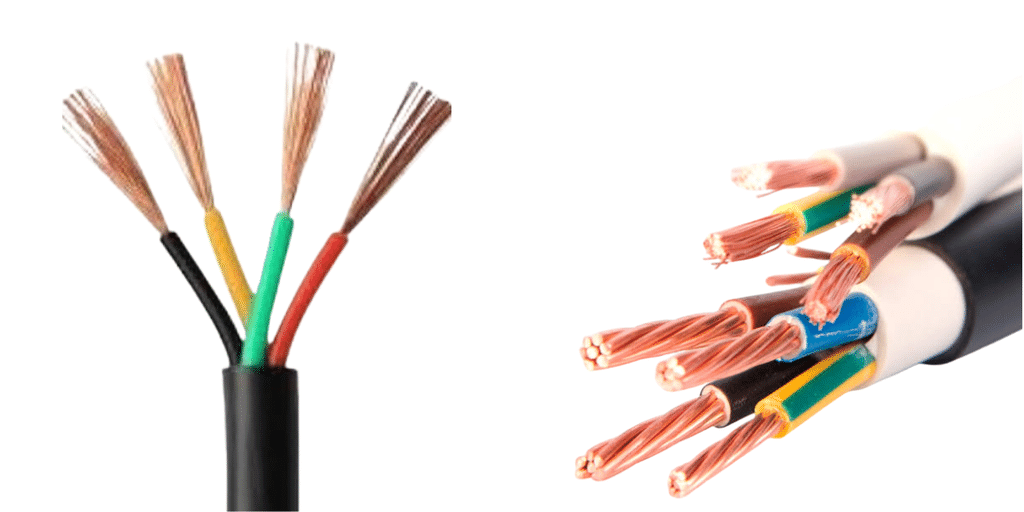
Multicore cables are electrical cables that contain two or more insulated conductors inside one protective outer covering. Each conductor carries electrical current or signals according to the cable’s intended application. The conductors are generally made from copper or aluminium, depending on the cable design and requirements.
The individual conductors are insulated to prevent unwanted electrical contact. An outer sheath protects the cable against environmental conditions and everyday wear, depending on its construction.
These are available in different conductor sizes, core configurations, insulation materials, and voltage ratings. The correct cable depends on the electrical load, installation environment, operating temperature, and application requirements.
For example, multicore cables can be used in industrial control panels, electrical machinery, automation systems, commercial buildings, and various equipment connections.
Growing Demand for Multicore Cables Manufacturers in India
India’s industrial and infrastructure sectors are growing rapidly. Manufacturing facilities, commercial buildings, power distribution systems, and automation projects require dependable electrical connections. This has increased the importance of choosing experienced multicore cable manufacturers and suppliers.
Customers generally look for products that provide consistent electrical performance, good insulation, mechanical strength, and long service life.
Indian manufacturers serve a wide range of industries, including engineering, construction, automotive manufacturing, electrical equipment production, and industrial automation. The availability of different cable specifications also helps buyers select products according to their project requirements.
When choosing a manufacturer, customers should consider product specifications, quality checks, technical support, applicable standards, and the manufacturer’s ability to meet their supply requirements.
Megacab can be considered by businesses looking for cable solutions suited to their electrical and industrial needs. Buyers should confirm the required cable specifications and product availability directly with the company before placing an order.
Types of Multicore Cables
Different applications require different multicore cable designs. Understanding the common types can help buyers make better purchasing decisions.
1. Flexible Multicore Cables
Flexible multicore cables are designed for applications where the cable needs to bend or move during normal operation. They are commonly used in machinery, portable equipment, and certain industrial installations.
Their flexibility depends on conductor construction, insulation, sheath materials, and the manufacturer’s design.
2. Industrial Multicore Cables
Industrial multicore cables are used to connect electrical equipment, machines, and control systems. Depending on their design, they may provide resistance to abrasion, oils, moisture, or other environmental factors.
Selecting the right cable helps support dependable operation in demanding industrial environments.
3. Control Multicore Cables
Control multicore cables transmit control signals between electrical devices, control panels, and machinery. They are frequently used in manufacturing plants, automation systems, and industrial equipment.
Some designs include shielding to reduce electromagnetic interference where required by the application.
4. Power Multicore Cables
Power multicore cables are designed to carry electrical power through multiple insulated conductors. They are used in suitable electrical distribution systems, equipment connections, and industrial installations.
The conductor size, voltage rating, insulation, and installation method must match the intended electrical load and applicable regulations.
5. Shielded Multicore Cables
Shielded multicore cables include a conductive shielding layer that helps reduce the effects of electromagnetic interference. They can be useful in instrumentation, control, and signal transmission applications where electrical noise may affect performance.
The need for shielding depends on the equipment, signal type, installation environment, and grounding arrangements.
Applications of Multicore Cables
Multicore cables are used in many industries because they allow multiple conductors to be installed within one cable assembly.
1. Manufacturing Industries
Factories use multicore cables to connect machines, motors, control panels, and production equipment. Proper cable selection helps maintain reliable electrical connections and supports efficient manufacturing operations.
2. Industrial Automation
Automation systems depend on communication and control signals between sensors, controllers, and machines. Suitable multicore cables help connect these components in an organised manner.
3. Construction and Commercial Buildings
Multicore cables may be used in suitable building electrical systems, equipment connections, and control installations. Cable selection must follow the building’s electrical design and applicable safety requirements.
4. Electrical Panels
Control panels contain various electrical components that require organised wiring. Multicore can reduce wiring complexity and make cable routing more manageable.
5. Machinery and Equipment
Industrial machinery often requires connections for power, control signals, and auxiliary functions. Depending on the equipment design, multicore can provide a practical connection solution.
6. Infrastructure Projects
Infrastructure developments may require cables for electrical equipment, control systems, and other supporting installations. The cable specification should match the environmental and operational requirements of each project.
Benefits of Using High-Quality Multicore Cables
Choosing the right multicore cable can offer several advantages for industrial and commercial applications.
1. Organised Wiring: Multiple conductors within one outer sheath help reduce cable clutter and simplify routing.
2. Space Saving: A single multicore cable may replace several separate cables where the electrical design permits, helping use installation space more efficiently.
3. Reliable Performance: Properly selected cables support consistent power transmission or signal transfer within their specified operating limits.
4. Mechanical Protection: Suitable insulation and outer sheathing help protect conductors against expected physical and environmental stresses.
5. Easier Installation: A suitable multicore cable design can simplify installation and cable identification, especially in machinery and control panels.
6. Reduced Maintenance Complexity: Organised cable routing can make inspection, troubleshooting, and maintenance more manageable.
7. Application Flexibility: Multicore cables are available in different core counts, conductor sizes, and insulation types to suit a wide variety of applications.
These benefits depend on choosing the correct cable and installing it according to the manufacturer’s instructions and relevant electrical standards.
How to Choose the Right Multicore Cable Manufacturer in India
Before purchasing multicore cables, businesses should evaluate several important factors.
- Product quality: Check conductor quality, insulation construction, and manufacturing consistency.
- Correct specifications: Confirm the number of cores, conductor size, voltage rating, and current-carrying capacity.
- Insulation material: Select insulation and sheath materials according to temperature, moisture, chemicals, and other site conditions.
- Safety and compliance: Verify relevant certifications, test reports, and applicable Indian or international standards for the intended application.
- Technical support: Choose a company that can help clarify product specifications and suitability.
- Supply requirements: Confirm availability, order quantities, delivery schedules, and commercial terms.
- Application suitability: Ensure the cable is designed for the intended use rather than selecting a product based on price alone.
A reliable purchasing decision considers the cable’s complete operating requirements, not simply its initial cost.
Why Choose Megacab for Cable Solutions
When searching online for Multicore Cables Manufacturers in India, buyers want a company that understands the importance of electrical performance, quality, and dependable service.
Megacab serves as the featured brand in this article for customers exploring cable solutions for industrial and electrical applications.
Here are some important considerations for businesses evaluating Megacab:
Focus on customer requirements: Understanding the project’s electrical and installation needs helps buyers identify suitable cable specifications.
Suitable product selection: Choosing the correct conductor size, core configuration, insulation, and sheath is essential for reliable operation.
Industrial application needs: Cable requirements can vary across manufacturing plants, machinery, electrical panels, and automation systems.
Quality-conscious purchasing: Buyers should confirm available test documentation, applicable standards, and product specifications before ordering.
Long-term value: Selecting a suitable cable can help support reliable operation and reduce avoidable installation or maintenance problems.
For current product availability, technical specifications, certifications, and quotations, contact Megacab directly through its official business channels. Confirm that the selected product meets your project’s requirements before installation.
Importance of Quality in Multicore Cable Manufacturing
Cable quality directly affects electrical safety and equipment performance. Poorly selected or incorrectly installed cables may experience overheating, insulation damage, signal interference, or premature failure.
Manufacturers should apply suitable quality-control procedures to ensure that products meet their specified requirements. Depending on the cable type, relevant checks may include conductor resistance, insulation performance, dimensional inspection, voltage testing, and sheath quality.
Buyers should also ensure that cables are installed by qualified personnel. Correct routing, bending radius, protection, termination, and load calculations are important for safe and dependable operation.
Choosing a suitable cable from a quality-conscious supplier helps businesses make informed decisions and maintain reliable electrical systems.
Frequently Asked Questions (FAQs)
1. What are multicore cables used for
Multicore cables are used for electrical power transmission, control signals, machinery connections, automation systems, and other applications requiring multiple insulated conductors.
2. How many cores can a multicore cable have
The number of cores depends on the cable design and application. Different configurations are available to suit specific electrical and control requirements.
3. Which insulation is commonly used in multicore cables
PVC is a common insulation material. Other materials may be used depending on temperature, chemical exposure, flexibility, fire performance, and environmental requirements.
4. How do I choose the right multicore cable
Consider the number of cores, conductor size, voltage rating, current capacity, insulation type, installation environment, and applicable standards.
5. Are multicore cables suitable for industrial automation
Yes, suitable multicore cables are widely used in automation systems for control and signal connections. The cable must match the equipment’s electrical and environmental requirements.
6. What should I check before buying multicore cables in India
Check product specifications, quality documentation, applicable standards, supplier reliability, delivery requirements, and compatibility with your application.
7. Why consider Megacab for multicore cables
Megacab is a brand to consider when evaluating cable solutions. Buyers should contact the company to confirm available products, technical specifications, and suitability for their projects.
Add a stronger Megacab call to actionInclude more India-focused buying questions
Conclusion
Multicore cables are an important part of modern electrical infrastructure. Their ability to carry multiple conductors within a common protective sheath makes them useful for industrial machinery, control panels, automation systems, commercial installations, and many other applications.
The growing demand for dependable electrical products has made Multicore Cables Manufacturers in India an important search category for industrial buyers, contractors, distributors, and equipment manufacturers.
When purchasing multicore cables, customers should consider conductor size, core count, insulation, voltage rating, operating conditions, and applicable standards. These factors help ensure that the selected cable meets the project’s technical and safety requirements.
Megacab is a brand to explore when evaluating cable solutions for your business. By identifying your requirements and confirming the available specifications with the company, you can make a more informed purchasing decision for your electrical and industrial projects.
Choose the right multicore cable for reliable connections, organised wiring, and long-term performance.